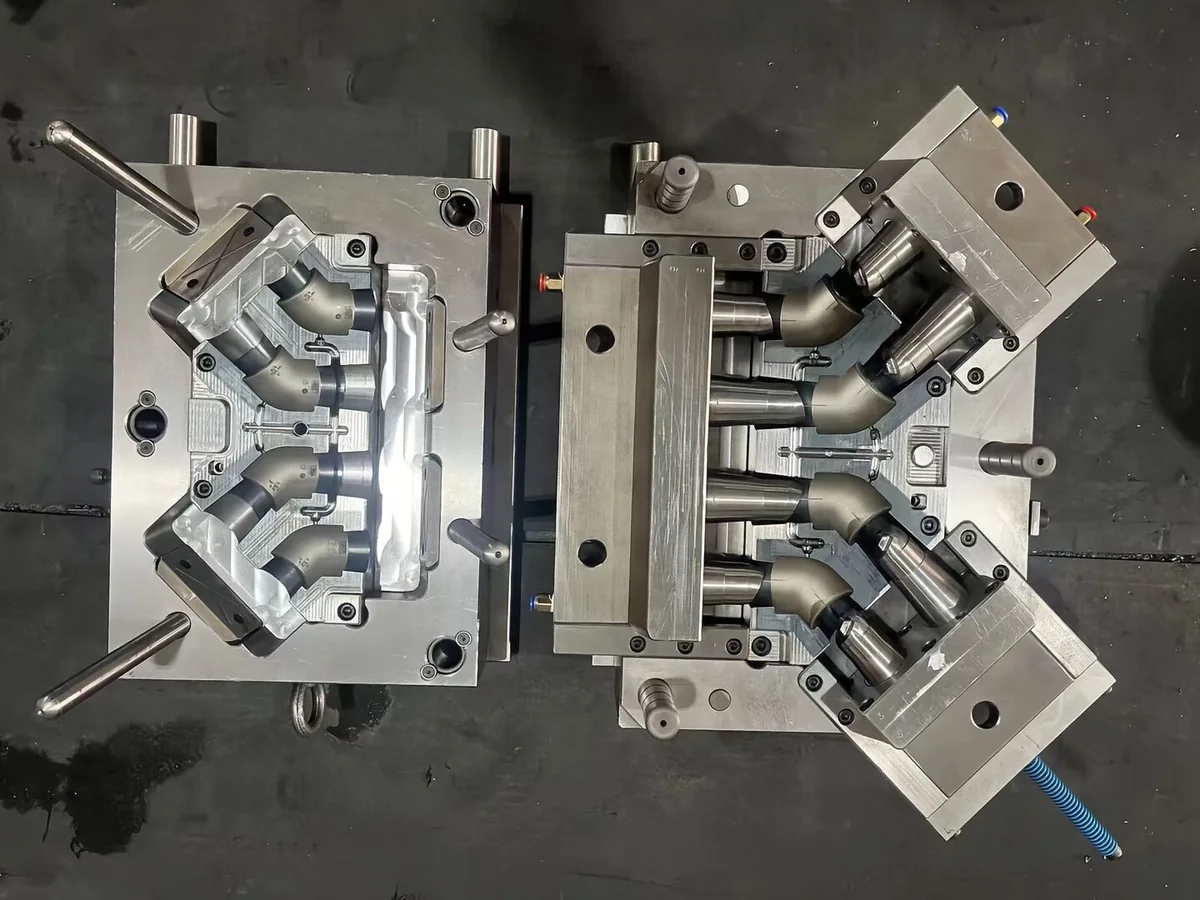
Photo context: This authorized four-cavity elbow mold photo is a project reference. It is not the part analyzed in the sample DFM excerpts below.
This guide helps buyers surface visible questions before an injection mold RFQ. It is not a rulebook for approving a plastic part or mold. A released CAD model and drawing can reveal where information is missing or where a supplier should look more closely, but they cannot by themselves establish filling behavior, pressure, cooling, warpage, core shift, weld-line performance, ejection reliability, or a stable process window.
Treat each red flag below as a prompt: record what is observable, identify the business or functional priority, and ask what part-specific review is needed. Do not turn a general draft, wall, or rib guideline into an acceptance criterion without the specified material, texture, geometry, process, and function.
What a buyer can check without running Moldflow
A buyer can review package completeness and mark visible conflicts without claiming to have completed engineering analysis:
- Revision: Confirm that every 3D file, 2D drawing, and specification identifies the same released revision.
- Pull direction: Mark the intended mold opening direction and any surfaces whose release direction is still undecided.
- Wall changes: Highlight abrupt thickness changes, thick pads, and transitions that are visible in the released geometry.
- Undercuts: Identify clips, holes, threads, hooks, or returns that appear to block straight-line release.
- Texture: Name the textured surfaces and state the required texture specification instead of relying on a rendered appearance.
- Cosmetic or sealing surfaces: Mark faces where gate witness, ejector marks, weld lines, sink, or flash would affect use or acceptance.
- Assembly constraints: State the mating parts, insertion direction, clearance needs, and interfaces that must remain accessible.
- Critical dimensions: Distinguish functional or inspection-critical dimensions from general drawing dimensions and name their datum or measurement basis.
These checks describe the released package. They do not predict how polymer will flow or how the proposed tool and process will behave.
Ten red flags and what to ask
| Risk | Visible clue in the released package | Why it matters | Question for the supplier |
|---|---|---|---|
| Draft | Faces appear parallel to the stated pull direction, or textured faces have no visible release allowance. | Release force, scuffing, or part damage can depend on material, texture, depth, and geometry. | Which faces need draft review for the proposed pull direction, texture, and resin? |
| Wall variation | Thick-to-thin transitions, isolated heavy sections, or thick pads are visible in the model. | Fill, pack, cooling, sink, and warpage behavior may become uneven. | Which wall transitions require simulation, coring, or geometry discussion before tool design? |
| Ribs and bosses | Deep ribs, heavy rib-to-wall intersections, or bosses tied into thick regions are visible. | Filling, sink, cooling, strength, and ejection trade-offs cannot be settled by a generic ratio. | Which rib and boss regions need section review, venting review, or local analysis? |
| Undercuts | Clips, side holes, threads, hooks, or returns interrupt straight-line release. | The tool may require slides, lifters, collapsible cores, unscrewing, or a geometry change. | What release concept is proposed, and which assumptions affect tool complexity or witness marks? |
| Gate-constrained surfaces | Cosmetic, sealing, assembly, or customer-facing surfaces leave few acceptable gate-witness locations. | Gate choice affects filling, packing, vestige, weld lines, and deformation. | Which gate regions are feasible, and what analysis is needed before selecting one? |
| Weld-line-sensitive functions | Flow fronts could meet near a snap, seal, hinge, fastener, pressure boundary, or visible face. | Weld-line location and strength depend on gate strategy, material, geometry, and process conditions. | Which functions need weld-line prediction or testing, and what acceptance criterion applies? |
| Long or slender cores | Deep holes, thin core pins, or long core features have limited apparent support. | Injection pressure and uneven flow can deflect a core and shift dimensions or wall balance. | Which cores need pressure and core-shift analysis, added support, or a different molding strategy? |
| Flatness or appearance without datum priorities | A flatness or appearance target is shown without functional datums, measurement setup, or ranked surfaces. | Warpage direction and cosmetic trade-offs cannot be judged against an unclear acceptance basis. | Which datums, measurement condition, and surface priorities will govern engineering review? |
| Texture near shut-offs | Texture reaches a parting line, shut-off, seal-off, or narrow release region. | Texture can change release needs and the feasibility of clean shut-offs or flash control. | Where should texture stop, and which shut-off faces need draft or tool-feasibility review? |
| Open resin, tolerance, or volume assumptions | Resin grade, tolerance basis, demand, cavity expectation, or production volume remains undecided. | These inputs change shrinkage, pressure, cooling, wear, process window, and tool architecture. | Which assumptions must be confirmed before DFM conclusions or the mold concept can be approved? |
There is no universal draft angle or rib ratio that this checklist can approve; material, texture, depth, geometry, gate, process, and function change the answer.
How to read the sample DFM annotations
The two excerpts below come from JF MOULD’s public sample DFM report. They show how review observations are presented. A marked image does not establish a corrected design, trial result, or customer acceptance.
Draft and release
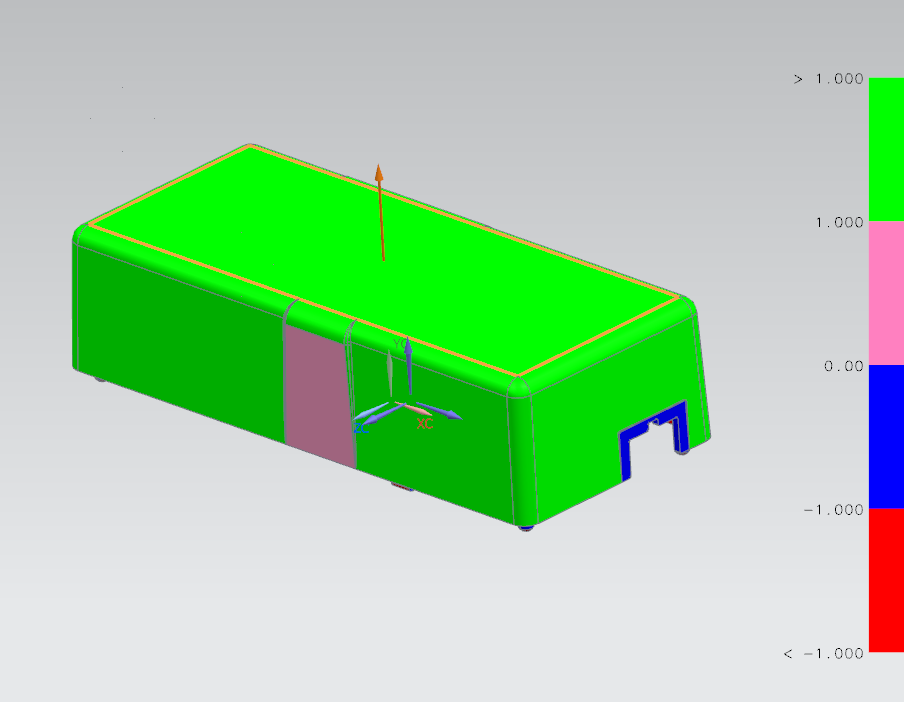
- Observed: Blue faces are flagged for no-draft review against the legend and pull direction.
- Decision: Agree the affected faces, resin, texture, and depth before proposing a draft change; the image sets no universal angle.
- Verification to agree: Recheck the revised draft analysis, then define trial checks for release and surface marks.
Wall-thickness transitions
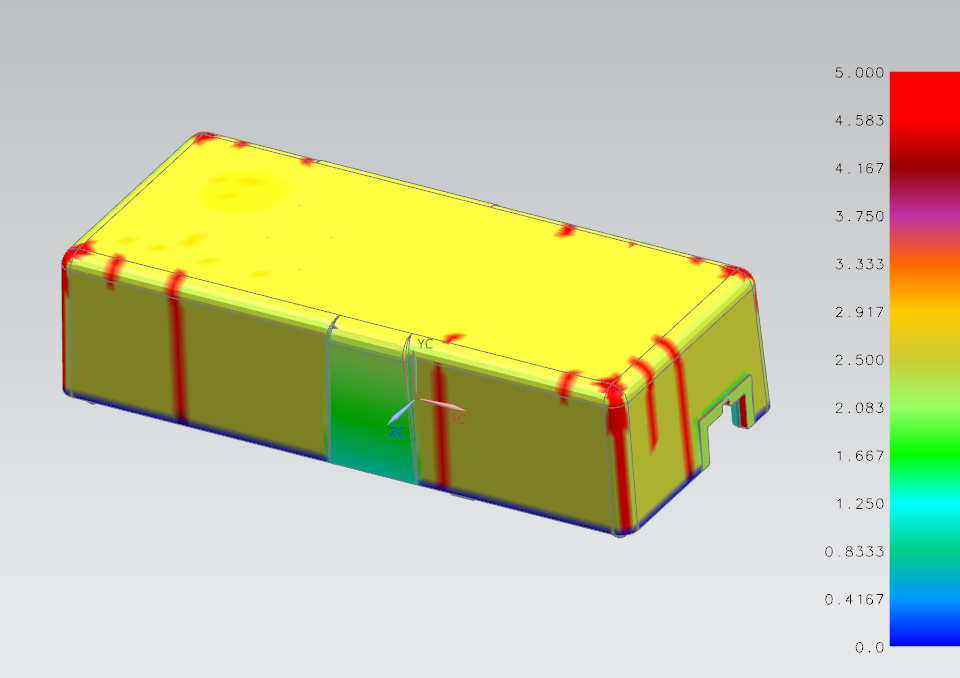
- Observed: Red regions mark thicker areas and prompt a sink-risk review.
- Decision: Discuss the marked transitions, material, and cosmetic or functional surfaces before proposing coring or another geometry change.
- Verification to agree: Compare the revised thickness map and define any needed filling, cooling, sink, and warpage analysis or trial checks; this image supplies no performance result.
View the public DFM sample and full report for the source context. Keep the proposed change and its drawing revision linked to the trial checks and open corrections.
When engineering analysis is required
The following questions require part-specific engineering inputs and a proposed molding or tool concept. Depending on the risk, the work may include simulation, calculations, tool-design review, material data, trials, or physical testing:
- Fill and pack: Evaluate whether the proposed gate and runner concept can fill and pack the part without unacceptable hesitation, short shot, or packing imbalance.
- Pressure: Estimate filling and packing pressure against machine capability, gate strategy, material, and core-loading risk.
- Cooling: Review circuit access, hot spots, temperature balance, and cooling-time drivers in the proposed tool layout.
- Warpage: Predict deformation using the specified material, fiber orientation where relevant, process assumptions, geometry, and acceptance datums.
- Core shift: Assess pressure imbalance and support for long, slender, or asymmetrically loaded cores.
- Weld lines: Predict likely locations and evaluate them against structural, sealing, cosmetic, or fatigue requirements.
- Ejection: Review release, friction, ejector placement, part stiffness, marks, and deformation after the mold concept is defined.
- Process window: Test whether acceptable parts remain feasible across realistic variations in material, temperature, pressure, time, and machine conditions.
A checklist can prioritize these questions; it cannot answer them or approve a mold. The supplier still needs the controlled geometry, resin grade, functional requirements, tolerance and measurement basis, expected volume, target equipment where applicable, and agreed acceptance criteria.
How this guide was prepared
This guide combines public technical references with JF MOULD’s perspective on organizing overseas RFQ communication. It is not a published project case study, and it does not replace part-specific DFM, material, quality, or tooling review.
Sources and further reading
- Autodesk Moldflow Adviser: Design Adviser analysis
- Draft Angle result
- How thickness affects flow
- ISO 20457: Plastics moulded parts — Tolerances and acceptance conditions
These public references help define analysis topics and tolerance context. They do not validate this checklist against a named customer project, approve a specific geometry, or replace an agreement between buyer and supplier.
To share these observations and open questions for part-specific review, use the manual injection mold RFQ form.
Next step
Turn this article into an RFQ review.
Send files or a project brief, material, annual volume, or target timing notes. Jessica and the engineering team will review manufacturability risk and reply with initial engineering feedback or quotation planning. First human reply targeted within 24 hours.